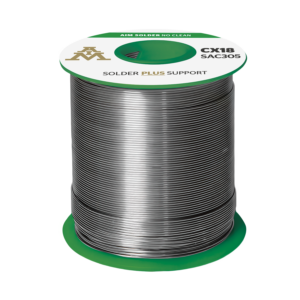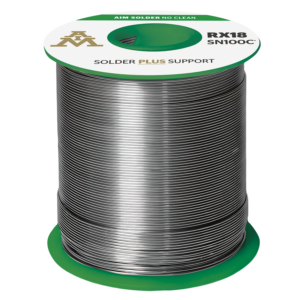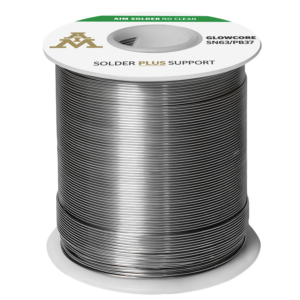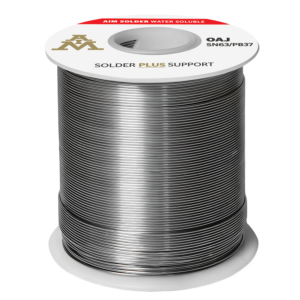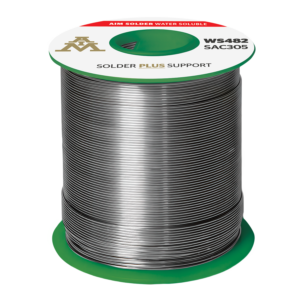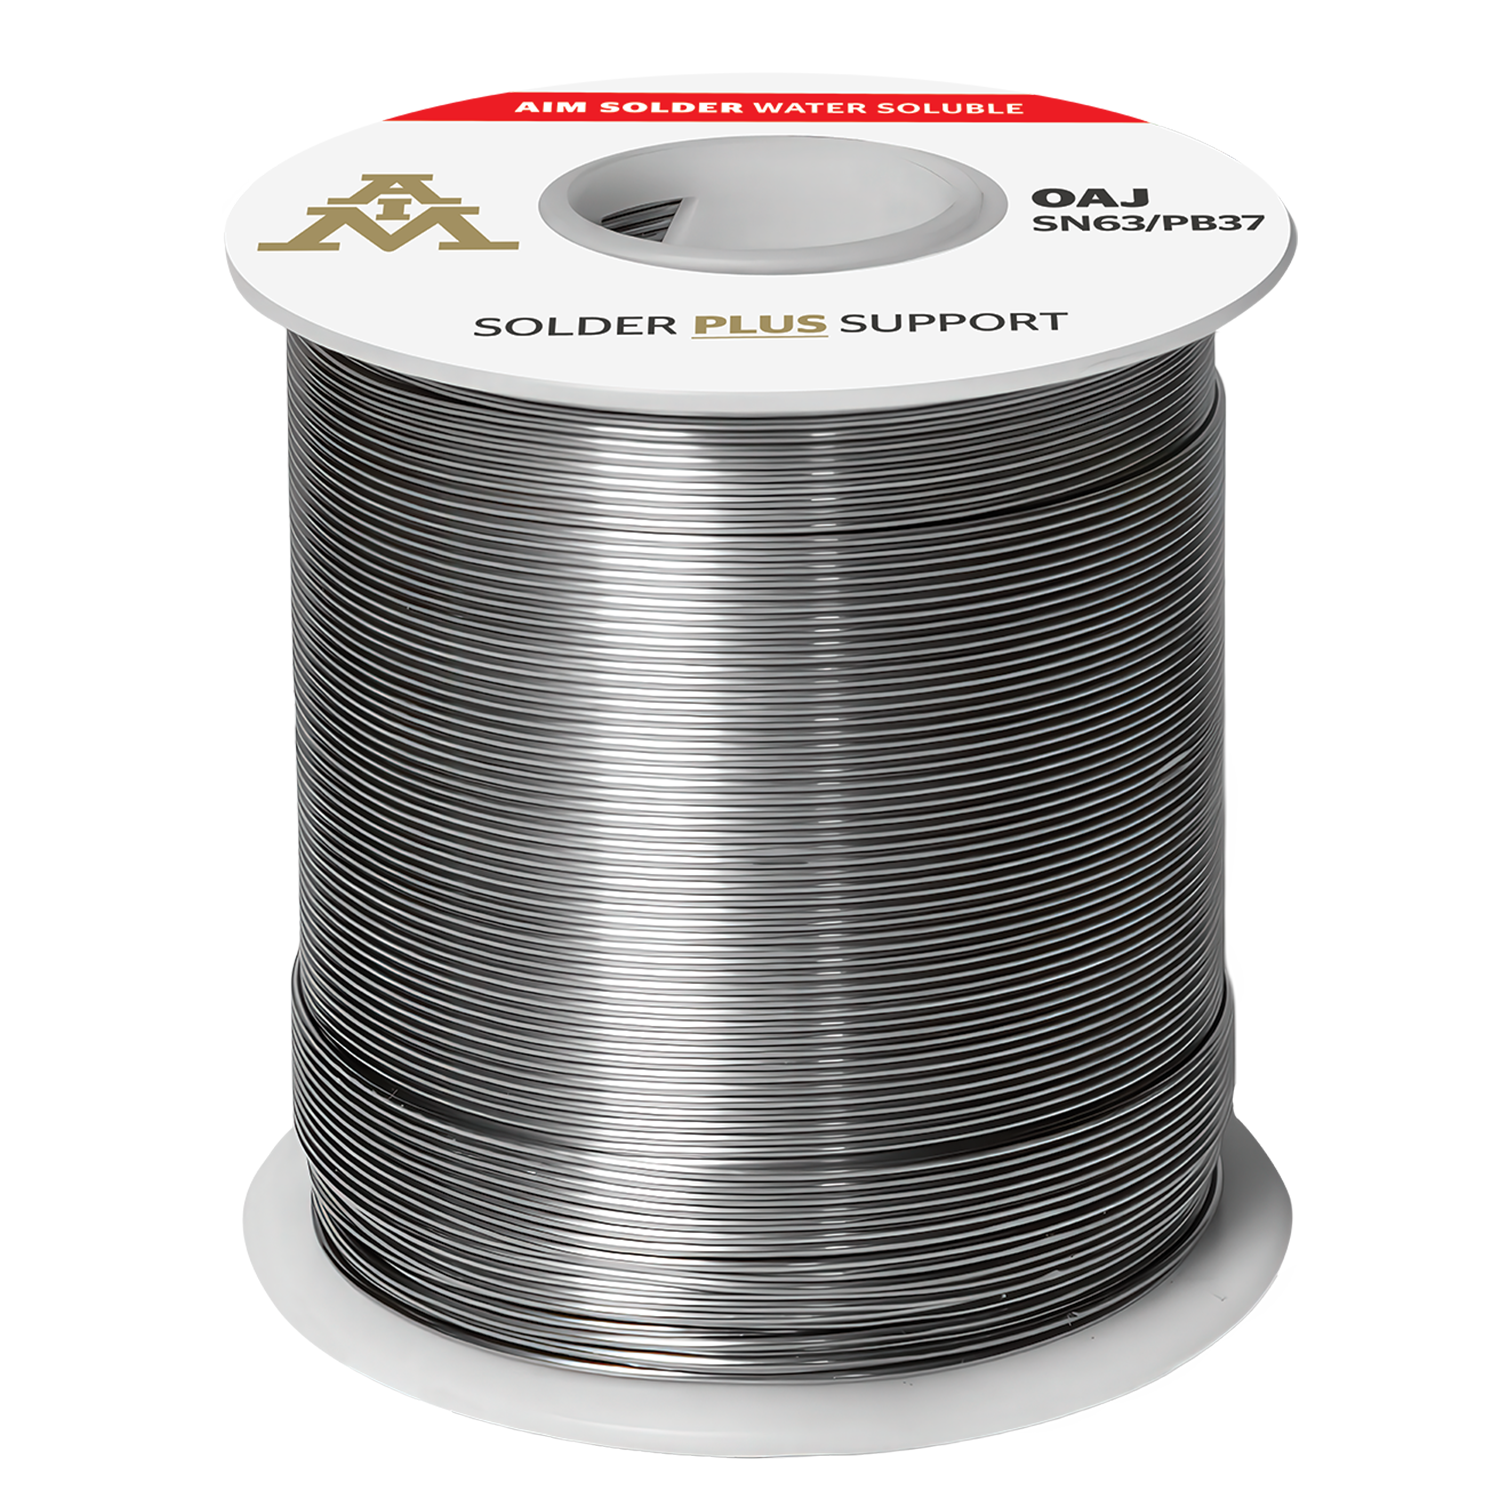
OAJ Cored Water Soluble Wire Solder

OAJ Flux Cored Solder Wire has been formulated with an innovative amine neutralized halide-activator system. This novel system offers a high activation level that provides rapid oxide removal and maximum capillary action, resulting in faster wetting on all surface finishes and plating. OAJ flux residues MUST be removed after soldering. IPC flux classification ORH1.
Excellent Wetting Properties, High Activity Level, Reduces Oxidation of Solder Iron Tip, Residue Washes Easily with DI Water Alone, Excellent Thermal Transfer.
OAJ Cored Wire is available in Sn/Pb, SAC305 and SN100C alloys. Other alloys, diameters and spool sizes may be available upon request.
Solder iron tip temperature should be between 350° – 400°C (650° – 750°F) for Sn63, Sn62 and Sn60 alloys, 370° – 425°C (700° – 800°F) for SN100C, Sn/Ag and Sn/Ag/Cu (SAC305, SAC405, CASTIN, etc.) alloys.
Store cored wire in a clean, dry area away from moisture and sunlight. Avoid freezing. 3 years at cool < 30°C (< 86°F) dry < 75%Rh
Post-process residues can remain in place up to 8 hours*. Flux residue can be removed with normal tap water @ 38° – 60°C (100° – 140°F) with a DI water final rinse. Use of a pressurized spray cleaning system is suggested, but is not required. *Environment and application dependent.
Use with adequate ventilation and proper personal protective equipment. Refer to the accompanying Safety Data Sheet for any specific emergency information. Do not dispose of any hazardous materials in non-approved containers.

Bulk Distribution & Commercial Supply

Built for volume distribution, our products are available for stocking wholesalers, retail suppliers, and commercial partners managing fleet or warehouse inventories. We support high-volume fulfillment, scalable ordering, and reliable supply chains for general-purpose repairs, maintenance, and commercial distribution. Reach out today to discuss contract pricing or regional distribution programs.