AIM-Industrial-horizontal-logo

Fil à souder à âme en résine Fastcore H

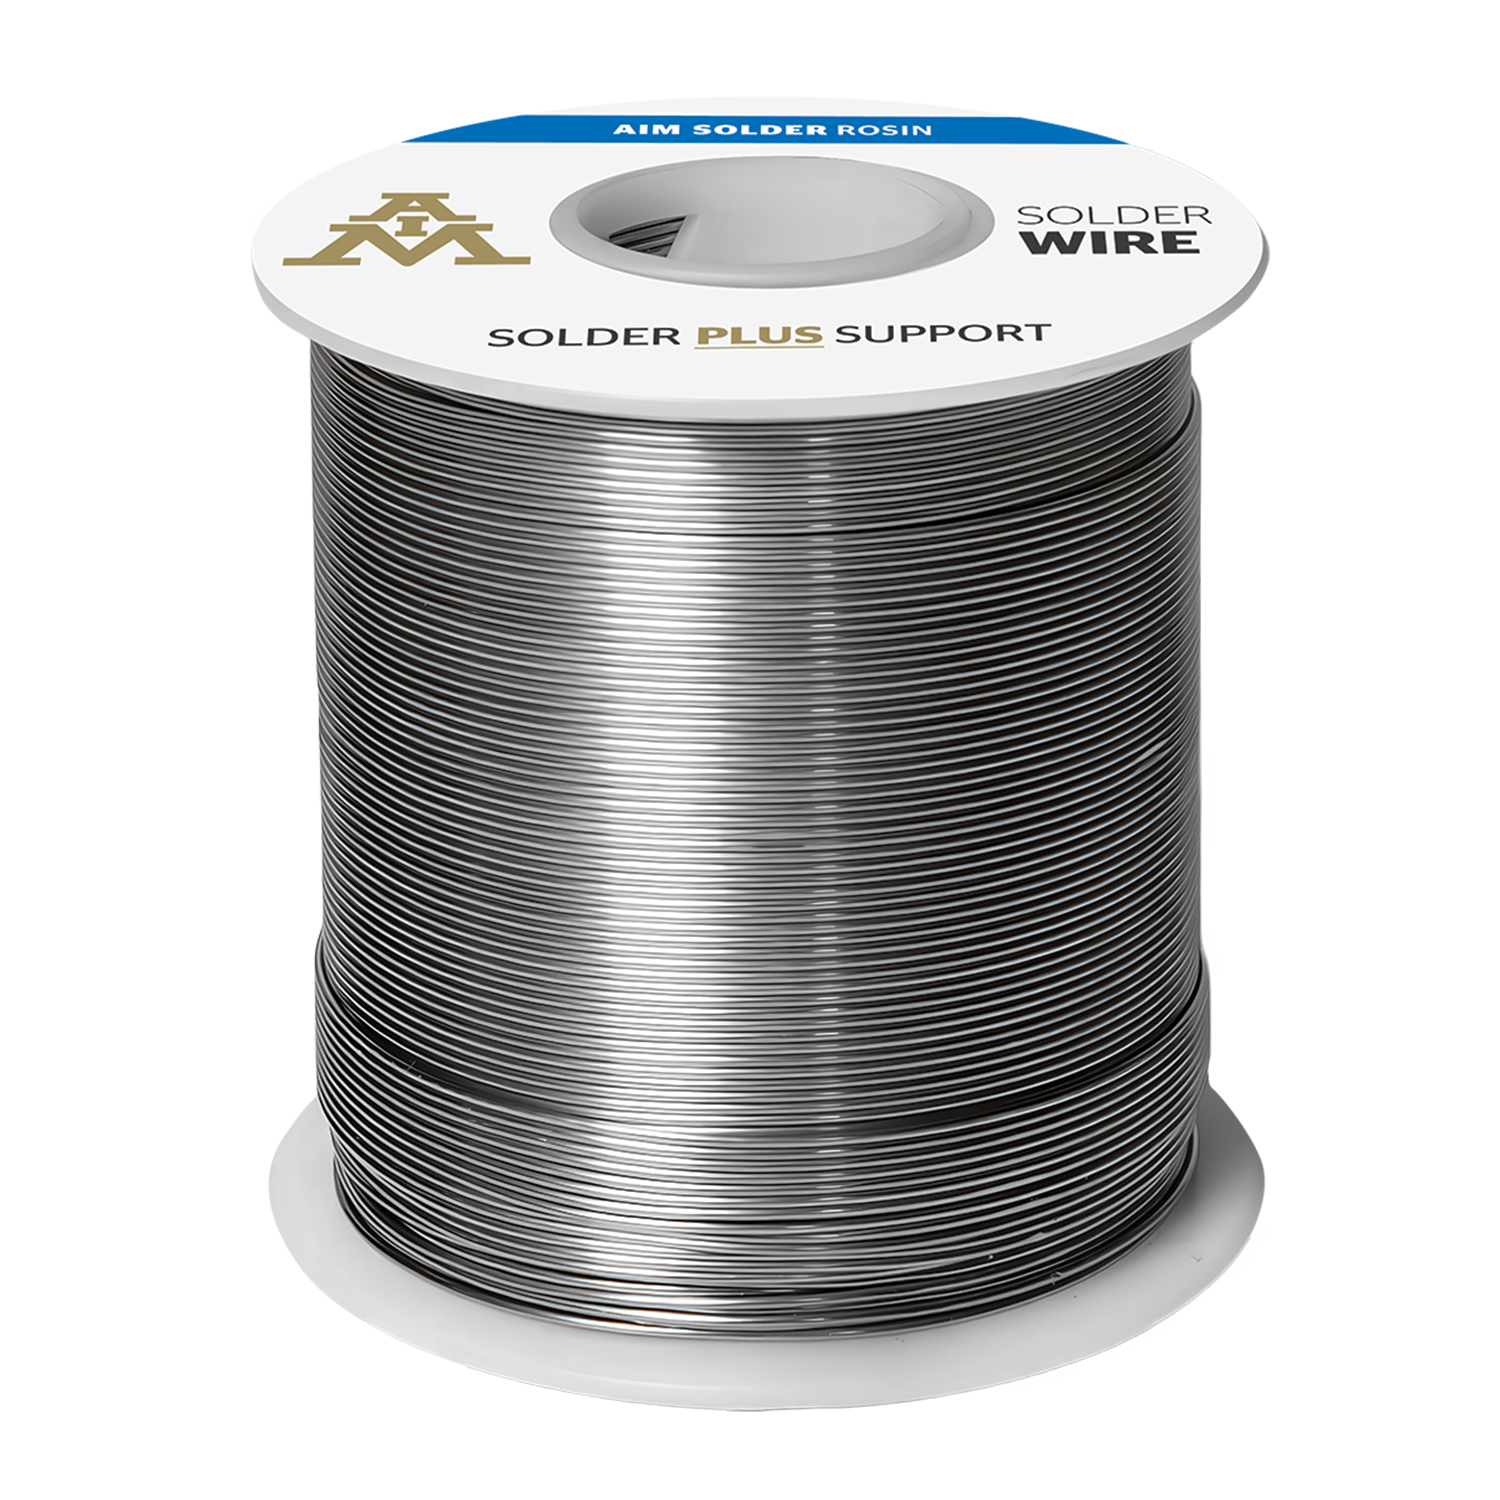
Fast Core H is a resin-based flux cored wire solder designed to offer excellent wetting characteristics, bright and shiny solder joints, and lead-free compatibility. This product is very active and is recommended for fast cycle time soldering. Fast Core H flux promotes good thermal transfer, offering excellent solder penetration into plated through holes or surface mount interconnections. Fast Core H produces low-to-medium, clear post-process residues. IPC flux classification for this material is REH1.
Excellent Wetting Properties, Produces Bright and Shiny Solder Joints, Wide Process Window, Clear, Hard Residues
Fast Core H is standard with a 2.5% flux core for tin-lead (2.5% flux core for lead-free) alloys. Available in Sn/Pb, Sn/Ag/Cu, SN100C? alloys. Standard spool sizes: ? lb. for .010 and .015 diameters; 1 lb. for .020, .032, .040, .050, and .062 diameters. Packaging of ? lb. and 1 lb. spools is standard in 12 lb. and 24 lb. cases. Other flux percentages, alloys, diameters and spool sizes may be available upon special request.
Solder iron tip temperature should be 350? – 400?C (650? – 750?F) for Sn63, Sn62 and Sn60 alloys, 370? – 425?C (700?- 800?F) for Sn/Ag and Sn/Ag/Cu alloys, 427? – 454?C (800?-850?F) for Sn10/Pb90 alloy, and 350? – 371?C (650?-700?F) for Sn43/Pb43/Bi14. Hold the solder iron at a 45? to 60? angle to the work surface. The solder iron should contact both the component lead and PCB pad surface. Solder and flux should flow onto both the lead and pad or lead and barrel to promote optimum flux activity to the joint being worked. If additional flux is needed, the use of AIM?s RA301 flux is recommended. Operators should use an applicator capable of dispensing precise amounts of flux to eliminate over-saturation and excessive spread.
Fast Core H wire has an indefinite shelf life when proper storage conditions are observed. Store product in a clean dry area away from moisture and sunlight. Do not freeze this product.
It is the decision of the user as to whether or not the cleaning of residues is required. If post-process cleaning is required, it is easiest if performed within a two to three hour period. A temperature of 100?-150?F normally is sufficient for removing residues. An in-line or other pressurized spray cleaning system is suggested, but is not required.
Use with adequate ventilation and proper personal protective equipment. Refer to the accompanying MSDS for any specific emergency information. Do not dispose of any hazardous materials in non-approved containers.

Distribution en gros et approvisionnement commercial

Conçus pour la distribution en gros, nos produits sont destinés aux grossistes, aux fournisseurs de détail et aux partenaires commerciaux chargés de la gestion des stocks de leur flotte ou de leurs entrepôts. Nous assurons la gestion des commandes en grand volume, un système de commande évolutif et des chaînes d'approvisionnement fiables pour les réparations courantes, la maintenance et la distribution commerciale. Contactez-nous dès aujourd'hui pour discuter des conditions tarifaires des contrats ou des programmes de distribution régionaux.