AIM-Industrial-horizontal-logo

Filo per saldatura con anima acida

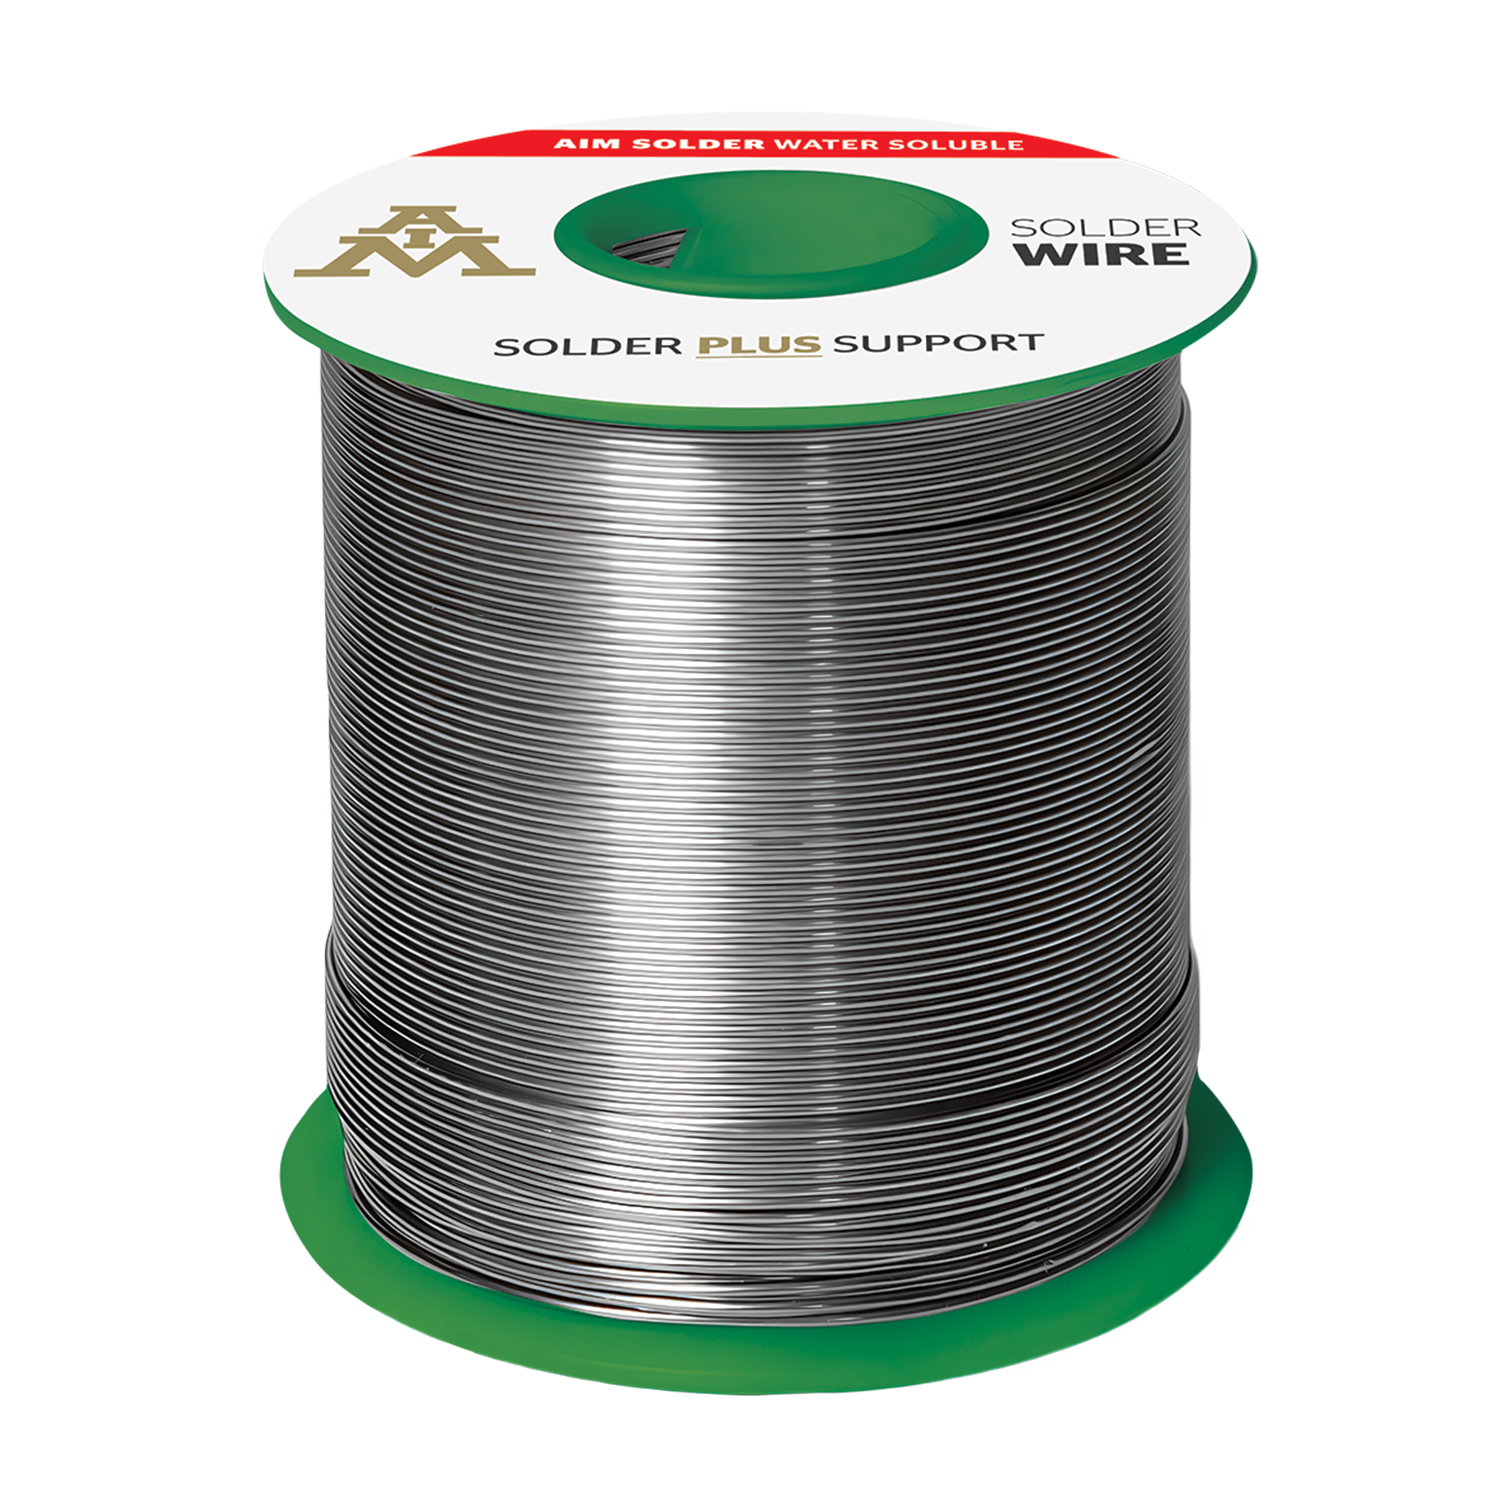
Acid Cored Wire features a halide-activated system that has been neutralized with an amine. The aminehydrohalide provides a high activation level that produces excellent tarnish or oxide removal, and maximum capillary action, leading to faster wetting, and reducing the chances of thermal degradation of the board materials. Remaining flux residue is readily soluble in hot water. IPC flux classification for this material is ORH1.
Improved Wetting Properties, High Activity Level, Good Thermal Transfer
Acid cored wire is standard with a 2% flux core. Other flux core %’s are available upon request. Available in Sn/Pb, Sn/Ag/Cu, SN100C® and other custom alloys upon request. These solder alloys are manufactured to meet the IPC J-STD-006 standard. Standard spool sizes; ½ lb. for .010 and .015 diameters, 1 lb. for .020, .032, .040, .050, and .062 diameters. Other spool sizes and wire diameters are available upon special request. Packaging of ½ lb. and 1 lb. spools is standard in 12 lb. and 24 lb. cases.
Solder iron tip temperature should be between 350° – 400°C (650° – 750°F ) for Sn60, Sn62 and Sn63 alloys, 370° – 425°C (700° – 800°F) for Sn/Ag and Sn/Ag/Cu alloys. Hold the solder iron at a 45° to 60° angle to the work surface. The solder iron should contact both the component lead and PCB pad surface. Solder and flux should flow onto both the lead and pad or lead and barrel to promote optimum flux activity to the joint being worked. If additional flux is needed, the use of AIM’s 715 flux is recommended. Operators should use an applicator capable of dispensing precise amounts of flux to eliminate over-saturation and excessive spread.
Acid cored wire has an indefinite shelf life when proper storage conditions are observed. Store product in a clean dry area away from moisture and sunlight. Do not freeze this product.
Post-process residues should be removed within a three-hour period. This may be accomplished with normal tap water. Deionized water is recommended for the final rinse. A temperature of 38º – 60ºC (100° – 140°F) is sufficient for removing residues. An in-line or other pressurized spray cleaning system is suggested, but is not required.
Use with adequate ventilation and proper personal protective equipment. Refer to the accompanying MSDS for any specific emergency information. Do not dispose of any hazardous materials in non-approved containers.

Bulk Distribution & Commercial Supply

Built for volume distribution, our products are available for stocking wholesalers, retail suppliers, and commercial partners managing fleet or warehouse inventories. We support high-volume fulfillment, scalable ordering, and reliable supply chains for general-purpose repairs, maintenance, and commercial distribution. Reach out today to discuss contract pricing or regional distribution programs.